Ribbon Mixer Working Principle: When to Use It vs Plow, Paddle, and V-Blender
· PerMix Team
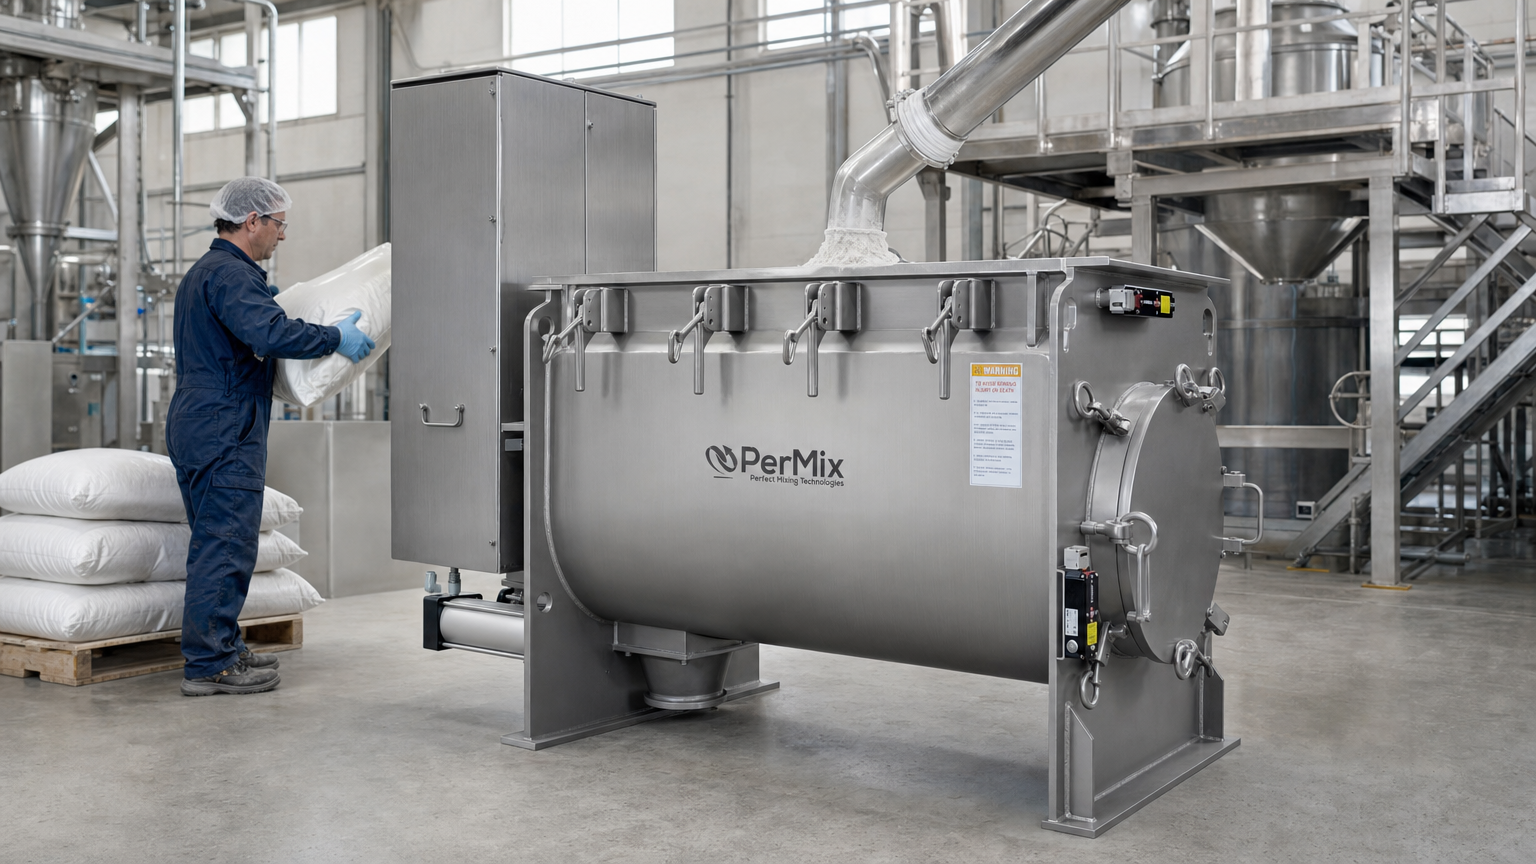
A ribbon mixer remains one of the most widely specified convective blenders for free-flowing powders and light granules. Understanding how the agitator moves material, and where that motion stops being enough, helps…
A ribbon mixer remains one of the most widely specified convective blenders for free-flowing powders and light granules. Understanding how the agitator moves material, and where that motion stops being enough, helps process teams avoid both under-mixing and unnecessary capital spend on more aggressive geometries.
How a ribbon mixer moves powder
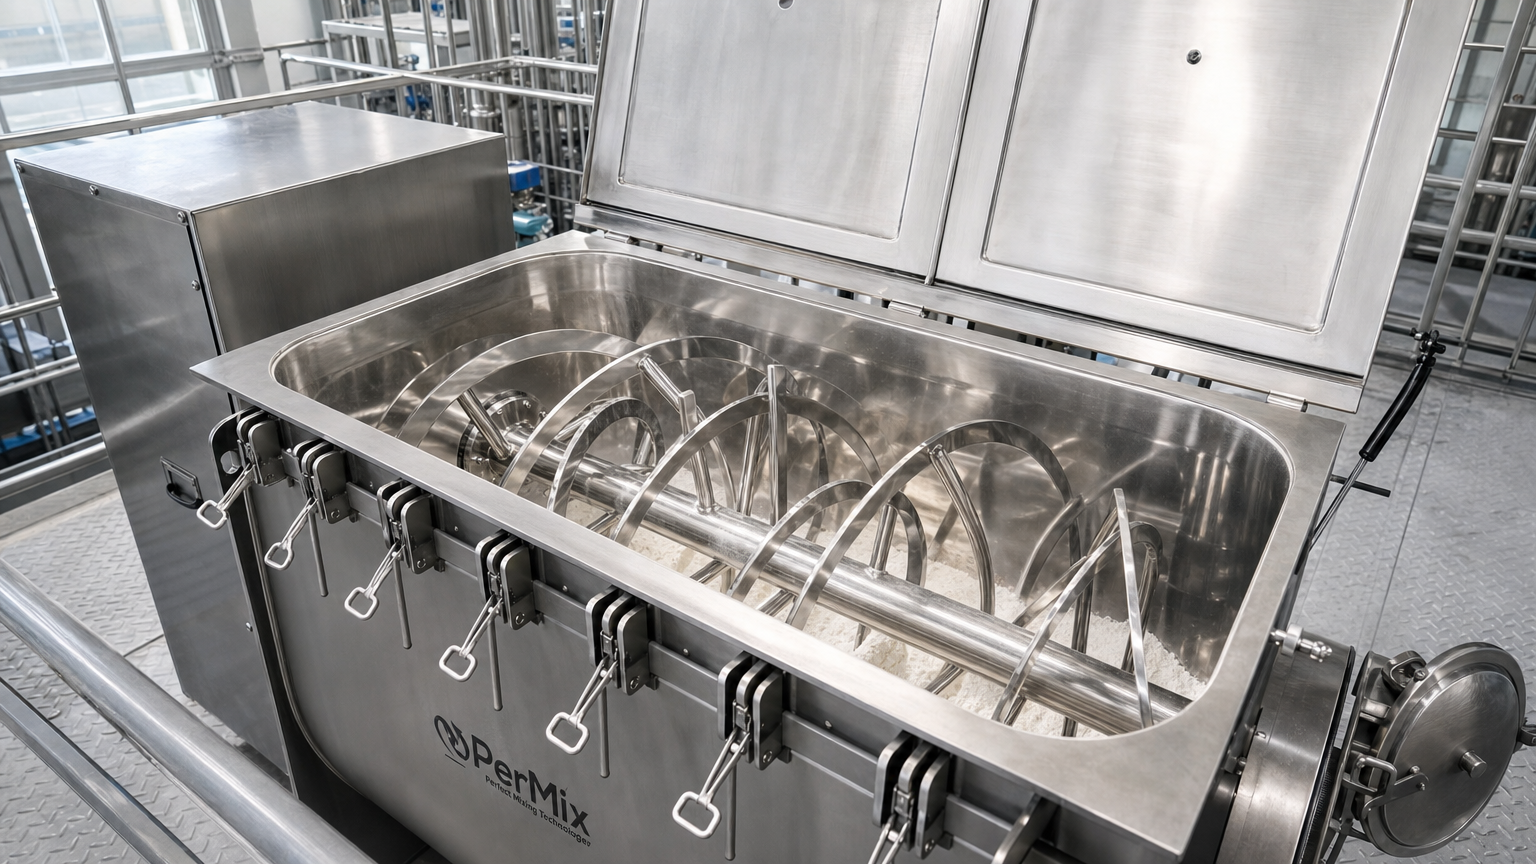
In a horizontal U-trough, inner and outer helical ribbons turn on a shared shaft. The outer ribbon typically conveys product in one axial direction; the inner ribbon returns it in the opposite direction. Combined with radial tumbling, that counterflow creates convective circulation along the trough length. Mixing time depends on fill level, ribbon pitch and diameter, rotational speed, and how freely the solids flow.
Unlike high-shear mills, a standard ribbon mixer relies on bulk motion rather than intense particle attrition. That suits duties where ingredients must stay intact, heat generation must stay low, and liquid addition is modest (often via spray bars timed into an established powder bed). Overfilling reduces the freeboard needed for turnover; underfilling can leave dead zones near the ends or under the shaft.
When a ribbon mixer is the right tool
Choose a ribbon mixer when:
- Powders are free-flowing or only mildly cohesive.
- Particle sizes and densities are not extremely mismatched.
- Target homogeneity is achievable in a few to several minutes at moderate tip speeds.
- Gentle handling matters more than rapid wet granulation or intensive de-lumping.
- Batch genealogy and flexible changeovers favor a batch vessel over continuous mixing.
Food premixes, nutraceutical blends, chemical additives, and many dry detergent or fertilizer bases fall in this envelope. For hygienic or validated environments, specify surface finish, seal type, and cleanout access together with capacity, as required for pharmaceutical and nutraceutical powder lines.
Ribbon mixers are not built to break hard cakes. If hygroscopic or compacted powders arrive with lumps, place a lump breaker on the mixer inlet so the batch is charged free-flowing.
Ribbon vs plow, paddle, and V-blender
Plow mixer
A plow mixer uses plow-shaped elements that lift and fluidize the bed at higher Froude numbers. It handles denser, more cohesive, or slightly sticky powders better than a classic ribbon and supports higher liquid addition rates. If your process needs mechanical fluidization or short cycle times on difficult solids, plow geometry usually outperforms ribbon.
Paddle mixer
Paddle mixer configurations trade some of the ribbon's axial conveying for adjustable paddle arrays. They help when you need tailored shear, easier cleanout of certain recipes, or intermediate duty between ribbon and plow. Compare options inside your industrial mixers shortlist rather than defaulting to the first familiar name.
V-blender (twin-shell)
V-blenders tumble the entire shell and excel at gentle blending of free-flowing pharmaceuticals and small-to-medium batches. They typically offer lower throughput for large campaigns and limited liquid incorporation. When campaigns are large and the plant standardizes on trough blenders, a ribbon mixer often wins on capacity and integration with existing powder handling.
For a wider comparison of tumble, convective and high intensity designs, read our powder mixer guide.
Common failure modes (and how to prevent them)
Incomplete homogeneity. Wrong fill level, insufficient mix time, poor liquid distribution, or post-discharge segregation. Fix the duty definition first; extra minutes rarely fix a geometry mismatch.
Shaft seal leakage and bearing contamination. Fine powders migrate. Specify seals, purge where needed, and schedule inspection, especially on abrasive products.
Ribbon deformation or fatigue. Dense or packed loads at high speed, or starting under a compacted heel, overload the agitator. Overload interlocks and correct start procedures matter as much as motor size.
Residue and cross-contamination. Dead zones at trough ends, under the shaft, or in discharge valves appear at production scale even when the pilot looked clean. Demand residue estimates and CIP/manual clean procedures in the RFQ.
Segregation after a "good" mix. Target CV in the vessel can still be lost in transfer. Evaluate hopper design, drop height, and pneumatic conveying separately from blender acceptance tests.
Scale-up tips that transfer from pilot to plant
- Hold similar fill fraction (percent of working volume), not only similar batch mass.
- Keep tip-speed or Froude regime in a proven band for that ribbon geometry; do not scale RPM 1:1 with diameter.
- Scale liquid addition by distribution quality (spray coverage, droplet size, addition window), not only by total kilograms.
- Record pilot mix time to a measured CV; production should reproduce the regime, then confirm with the same assay method.
- Design discharge and cleaning into the scale-up package. PerMix ribbon mixer designs typically pair capacity with agitator and outlet options for this reason.
See the PerMix ribbon mixer
Review capacities, agitator options, and outlets on the PerMix ribbon mixer product page. For cohesive powders that outgrow ribbon duty, compare the plow mixer and paddle mixer. For gentle tumble blending, see the V blender or double cone mixer.
Spec checklist before you buy
Ask for working volume vs total volume, recommended fill range, installed power, speed range, ribbon configuration, materials and finish, seal type, discharge valve size, and expected mix time for your recipe class. Among industrial mixers, ribbon geometry earns its place when solids are cooperative and the plant values predictable, gentle convective blending, not when the product needs intensive plow action or tumble-only aesthetics. Get the principle and the limits clear, and the machine stays a reliable workhorse instead of a chronic bottleneck.